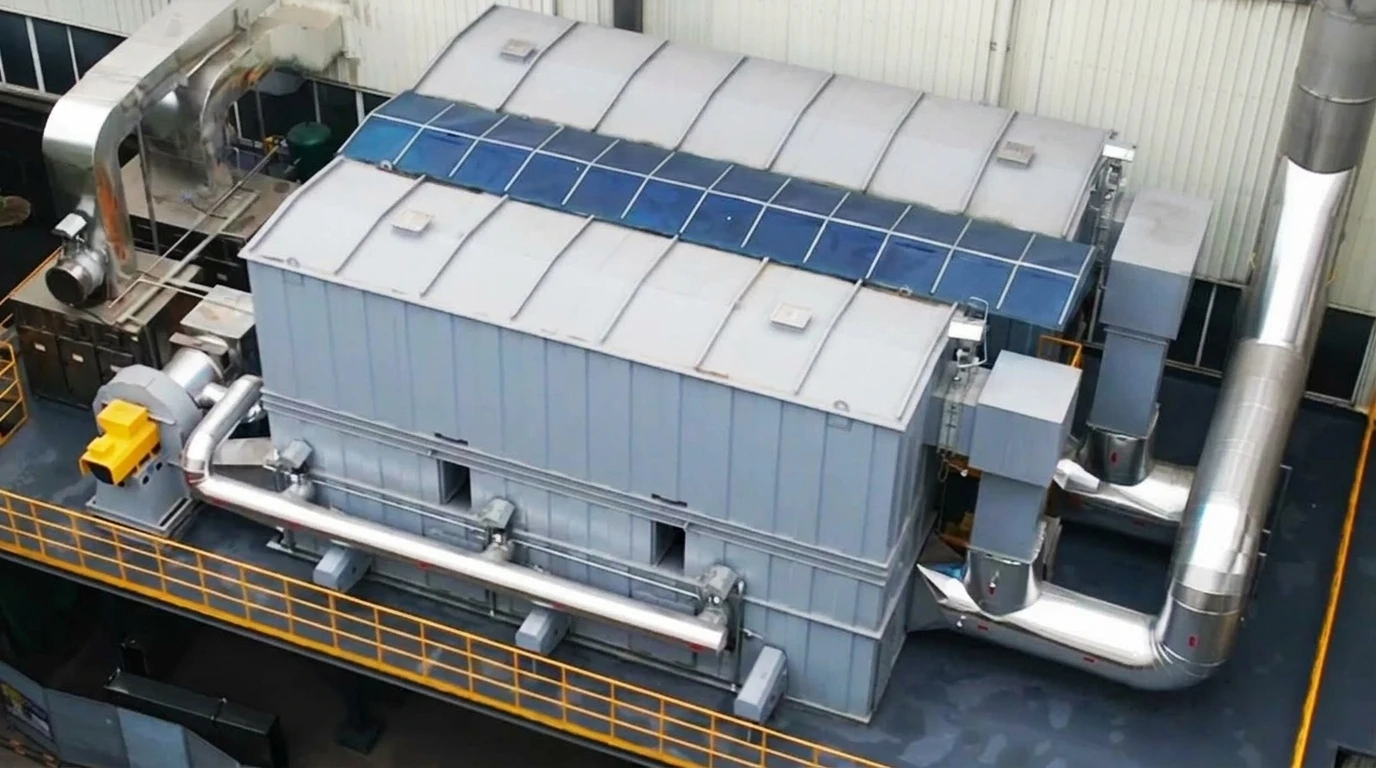
60,000 m³/h Dual 3-Bed RTO High-Efficiency Thermal Abatement System
Haier Smart Home Co., Ltd. (Chongqing) | Air Conditioner Heat Exchanger Degreasing Ovens
High-Temperature Stamping Lubricants in Smart HVAC Lines — Neutralized by Dual 3-Bed RTO
At the high-volume HVAC manufacturing center of Haier Smart Home in Chongqing, automated continuous production lines produce high-efficiency residential and commercial air conditioning systems. A critical thermal phase involves passing stamped aluminum fins and expanded copper tube assemblies (evaporator and condenser coil assemblies) through continuous degreasing furnaces operating at 200°C to 380°C. This process volatilizes residual evaporative stamping lubricants, drawing oils, and anti-corrosion additives into a dense, high-temperature stream laden with heavy hydrocarbons and sub-micron oil mist aerosols.
The legacy pollution control facility — consisting of a cyclone water scrubber, cooling tower, electrostatic oil precipitator, and UV photolysis — failed repeatedly. Volatile drawing lubricants rapidly cooled and condensed inside delivery ducts, creating dangerous liquid oil accumulation and fouling downstream electrostatic electrodes, triggering frequent maintenance shutdowns and constant risk of regulatory non-compliance.
FluxFine delivered a complete turnkey EPC solution: an elevated dual-train 60,000 m³/h (35,300 CFM) Three-Tower Regenerative Thermal Oxidizer (3-Bed RTO) system. Mounted on a customized 30-metric-ton heavy structural steel platform on the plant roof, the installation operates two dedicated oxidizer lines: a 35,000 m³/h (20,600 CFM) train for evaporator lines and a 25,000 m³/h (14,700 CFM) train for condenser lines, discharging through a unified 25-meter (82 ft) SUS304 stack. Utilizing Lantek structured honeycomb ceramic monoliths, automated soft-seal poppet switching valves, and FM-certified low-NOx burners, the facility achieves a verified ≥99.0% VOC Destruction and Removal Efficiency (DRE) and ≥95% Thermal Energy Recovery (TER), completely eliminating oil re-condensation fire risks in ductwork and reducing cold-restart energy demand by 65%.
Engineered Performance & Economic Benchmarks
By substituting troublesome legacy scrubbers with dual 3-bed regenerative thermal oxidation, Haier secured absolute environmental compliance alongside profound operational energy savings.
Destroys volatile paraffinic stamping hydrocarbons, ester lubricants, and aroma solvents at 760°C–850°C with continuous clean-gas purge.
Outperforms Chongqing DB50/418-2016 emission limit (50 mg/m³) by 60%, delivering future-proof municipal regulatory compliance.
60 m³ Lantek structured honeycomb ceramic monoliths store and recycle combustion heat, achieving self-sustaining auto-thermal state at ≥1.7 g/m³.
High-density ceramic bed retains ≥500°C after 24-hour idle periods, cutting cold-restart heating consumption by 65%.
Three Severe Engineering Obstacles Solved
Air conditioner heat exchanger coil degreasing involves harsh thermodynamic and spatial constraints that defeat standard off-the-shelf air pollution hardware.
Stamping Lubricant Aerosols & Pipe Clogging
Aluminum fin punching and copper pipe expanding require specialized volatile drawing lubricants. Discharged at 200°C–380°C, these heavy hydrocarbons cool rapidly in uninsulated ducting, condensing into viscous oil sludge that blinds ceramic media and creates catastrophic factory fire hazards.
Flexible Lean Shifts & Intermittent Cooling
Haier operates responsive pull manufacturing schedules. Ovens alternate dynamically between high-throughput batching, tooling changeovers, and overnight idling. Conventional incinerators consume excessive auxiliary natural gas keeping cold combustion chambers heated during intermittent pauses.
Zero Ground Footprint & Rooftop Structural Rigging
The A02 building perimeter is densely populated with press bays, material conveyors, and electrical substations. The entire 60,000 m³/h system had to be elevated onto the building roof, requiring full structural load recalculation, vibration isolation for heavy blowers, and storm-wind reinforcement.
Dual-Train Pre-Demisting & Thermal Regeneration
Two completely autonomous oxidizer trains decouple evaporator and condenser production, allowing Haier to throttle down unneeded capacity and eliminate pipeline thermal backflow.
Insulated SUS304 Ducting
1.2mm SUS304 piping insulated with 50mm rockwool preserves gas heat above condensation temperatures. Continuous slope gradients route accumulated liquids to sealed knockout oil traps.
Stainless Demister Boxes
Twin SUS304 filter vessels packed with 21 sets of multi-layer knitted wire mesh demister pads intercept ≥98% of oily aerosols (>3 μm) at 2.0 m/s face velocity before the RTO inlet.
Dual 3-Bed Regenerative RTO
Lantek structured honeycomb ceramics absorb and release heat with ≥95% TER. Combustion at 760°C–850°C decomposes organics into pure CO2 and H2O with zero valve-puff spikes.
Clean Stack & Energy Loop
Purified flue gas discharges via a 25 m tall SUS304 stack at ΔT < 40°C above ambient. Automated Modbus-RTU telemetry continuously reports emissions directly to plant SCADA.
Heavy-Duty Hardware Built for Rigorous Service
Every machine module reflects industrial-grade metallurgy, thermal durability, and failsafe pneumatic architecture designed for continuous 24/7 manufacturing.
Dual 3-Bed RTO Assemblies
- Heavy Corrugated Casing: 6.0 mm carbon steel shell eliminates exterior stiffeners and corrosion pockets.
- 250mm Ceramic Insulation: 192 kg/m³ density aluminum-silicate fiber holds outer skin ≤65°C.
- Pneumatic Poppet Valves: Soft-seal design with leakage ≤0.05% and >1,000,000 cycle lifespan.
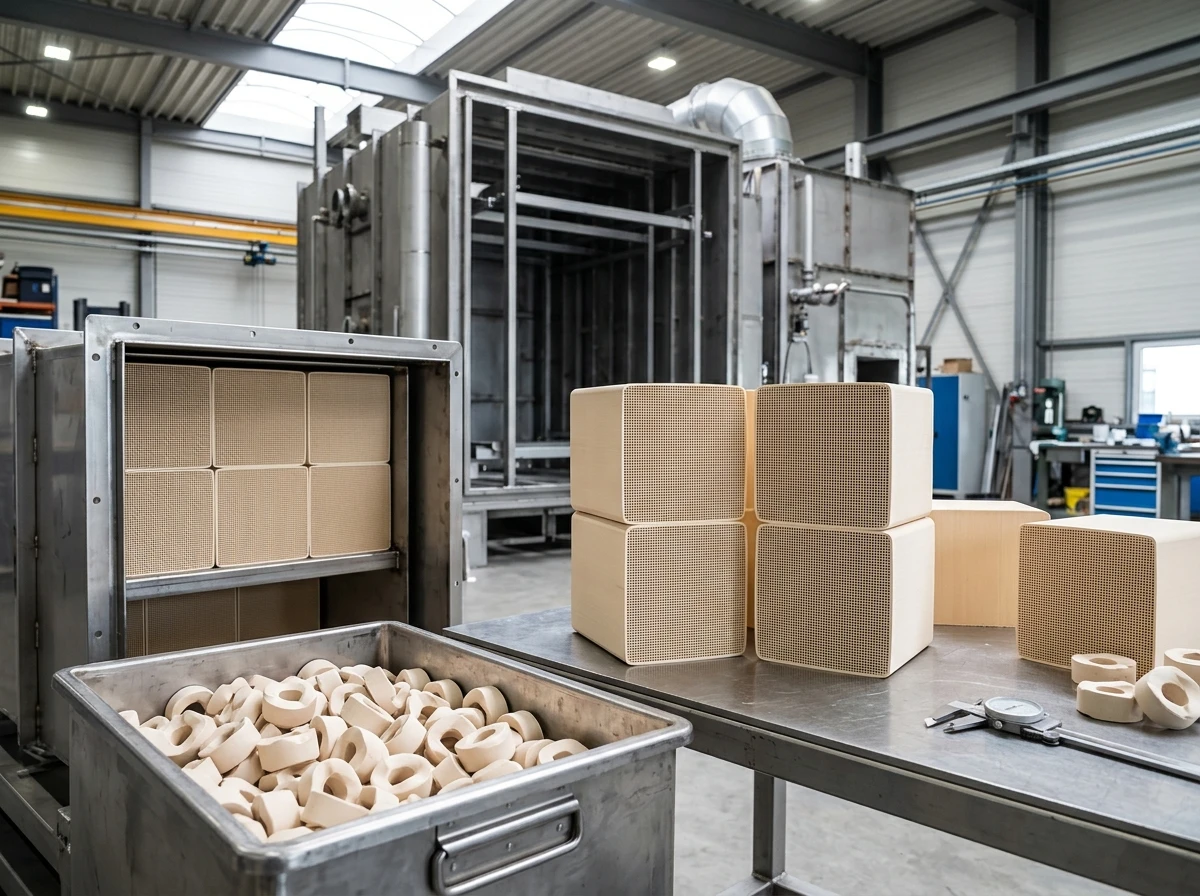
Lantek Honeycomb Ceramics
- Structured Monoliths: 150×150×150 mm blocks deliver ≥95% thermal recovery efficiency.
- Saddle-Ring Top Layer: R51 ceramic saddles distribute incoming air evenly and resist particulate blinding.
- 1,200°C Thermal Rating: High thermal shock resistance tolerates rapid valve switching cycles.
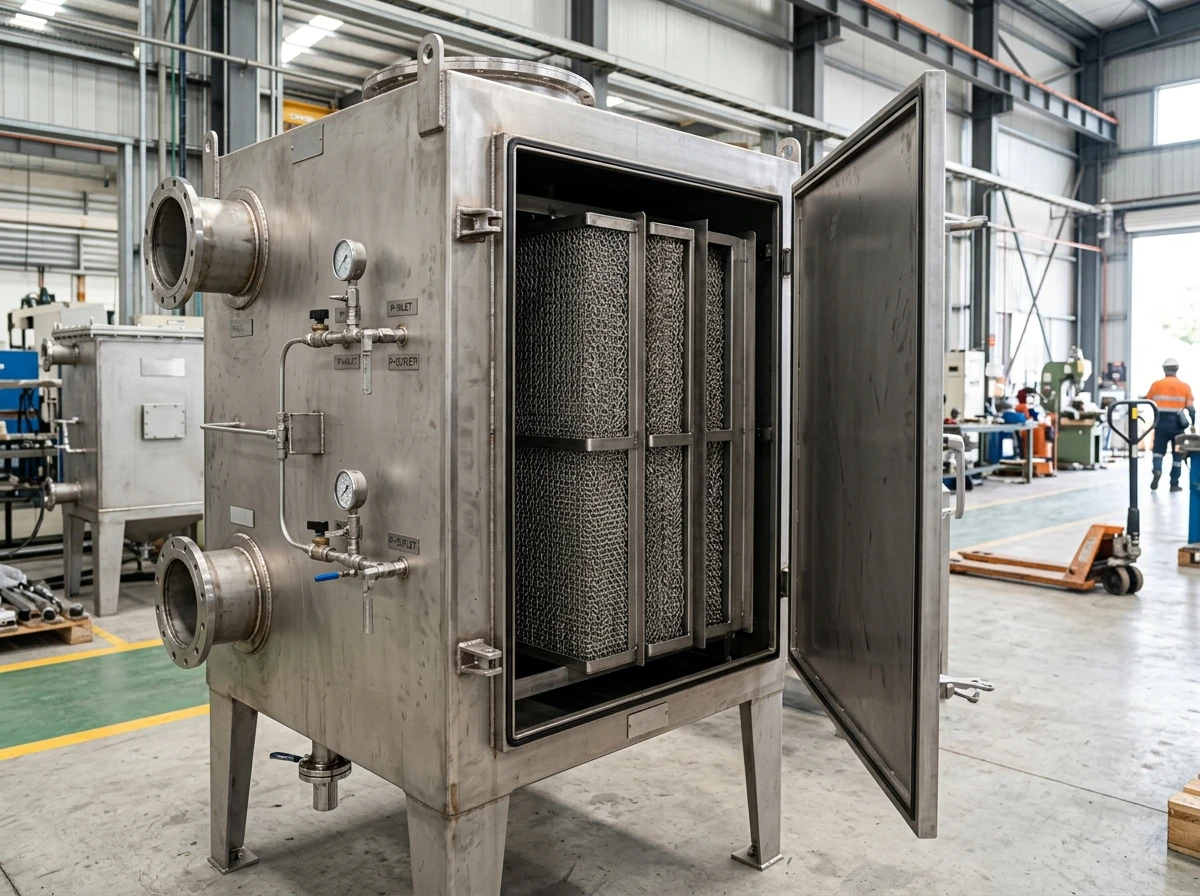
SUS304 Demister Pre-Filters
- Knitted 304 Mesh: 21 sets of 75mm stainless steel demister packs knock out ≥98% of oily aerosols.
- Differential Monitoring: Dwyer 4-20mA pressure transmitters alert operators prior to filter saturation.
- Integrated Thermal Jacketing: 50mm rockwool insulation prevents surface heat loss and condensation.
Four-Dimensional Rigorous Performance Specifications
Audited engineering data matching the technical URS contract across operating boundaries, emissions, energy economics, and safety.
Dimension 1: Inlet Operating Conditions & Design Boundaries
| Process Parameter | Engineering Specification | Dual Train Dimensioning | Operating Tolerance |
|---|---|---|---|
| Total System Airflow | 60,000 m³/h (35,300 CFM) continuous capacity | 35k m³/h (Evap) + 25k m³/h (Cond) | VFD Rated 120% Margin |
| Inlet VOC Concentration | 1,200 – 3,500 mg/m³ (variable by stamping speed) | Hydrocarbon + synthetic drawing oils | <25% LEL Safety Ceiling |
| Gas Stream Temperature | Oven exit: 200°C–350°C; RTO inlet: 70°C–110°C | 50mm rockwool insulated ductwork | Above Dewpoint (>65°C) |
| System Static Pressure | Central duct negative pressure: 200 – 500 Pa | Dual high-pressure fans (4,000–5,000 Pa) | ±50 Pa Pressure Stability |
Dimension 2: Guaranteed Environmental Compliance & Stack Limits
| Regulated Pollutant | Standard Regulatory Threshold | Haier URS Contract Limit | FluxFine Verified Emission |
|---|---|---|---|
| Destruction Efficiency (DRE) | Chongqing municipal baseline: ≥90.0% | ≥98.0% contract threshold | ≥99.0% (Average 99.3%) |
| Non-Methane Hydrocarbons (NMHC) | Chongqing DB50/418-2016: 50 mg/m³ | ≤35 mg/m³ (70% of standard) | ≤20 mg/m³ (EU BAT Standard) |
| Particulates & Oil Mist | Industrial Furnace DB50/659-2016: 30 mg/m³ | ≤21 mg/m³ (70% of standard) | ≤10 mg/m³ Ringelmann < Grade 1 |
| Odor Concentration | China GB14554-1993: ≤70 OU (dimensionless) | ≤49 OU (70% of standard) | ≤20 OU (Zero Perimeter Odor) |
Dimension 3: Thermal Efficiency, Auto-Thermal State & Heat Recovery
| Thermal Engineering Parameter | Conventional Incinerator | FluxFine Dual 3-Bed RTO | Operational Superiority |
|---|---|---|---|
| Thermal Energy Recovery (TER) | Direct thermal / catalytic: 60% – 75% | ≥95.0% (Lantek Honeycomb) | ≥95% Heat Recovery / Minimal Energy Need |
| Auto-Thermal Threshold | Requires natural gas continuously | Self-sustaining at ≥1,700 mg/m³ | Zero Auxiliary Fuel in Steady Production |
| Intermittent Pause Heat Retention | Cools down to ambient in 6–8 hours | Retains ≥500°C after 24 hours | 65% Restart Energy Saved |
| Cold-Start Warm-Up Speed | Requires 3–4 hours ramp-up (>300 kWh) | ≤60 minutes ramp-up (≤110 kWh) | < 1h Shift Readiness vs. 4h Industry Norm |
Dimension 4: Metallurgy, Structural Sizing & Safety Engineering
| Component / Safety Area | Engineering Material & Metallurgy | Design Specification | Safety Classification |
|---|---|---|---|
| RTO Outer Shell & Frame | Q235B 6.0 mm corrugated steel plate + 10# H-beam | Continuous full penetration weld | Zero Gas Leakage Housing |
| Internal Thermal Insulation | 250mm thick ceramic fiber (192 kg/m³, 1,260°C) | Heat-resistant stainless anchor studs | Skin Touch ≤ 65°C |
| High-Temp Emergency Dump Valve | AISI 310S ultra-high temperature stainless steel | Φ300mm fail-safe pneumatic opening (<0.5s) | UPS Power Loss Failsafe |
| Explosion & Flame Arresters | SUS304 corrugated crimped metal ribbon flame cells | Φ850mm & Φ700mm detonation proof | NFPA 68 / 69 Certified |
Automated PLC Logic & Triple Thermal Safeguards
A triple-tier safety loop interlocks oven production, gas supply, and exhaust bypasses to guarantee fail-safe plant continuity.
Online LEL & Temperature Array
Continuous Qi'an LEL combustible detectors analyze inlet gas streams. 11 thermocouple probes per RTO map bed thermal profiles, transmitting 4-20mA signals into the PLC to throttle burner firing and fresh-air dilution.
- Audible-visual alarm at 20% LEL
- Fresh-air dilution damper opens at 25% LEL
Dual Siemens PLC Controllers
Redundant PLC logic coordinates the overlapping cycle timing of pneumatic poppet valves, eliminating transient backpressure spikes that could force oily fumes back into the stamping workshop.
- Overlapping poppet valve timing (zero dead-head)
- Production interlock halts ovens if RTO faults
Emergency Dump & Explosion Vents
If utility power fails or chamber temperatures exceed 950°C, spring-loaded 310S bypass valves dump raw gas safely to stack within 0.5s via UPS power. Certified explosion rupture disks vent potential pressure waves harmlessly upward.
- 0.25 m² stainless rupture diaphragms
- 280°C fire dampers with remote telemetry
Global EPC Delivery for World-Leading HVAC Manufacturers
The successful delivery of Haier Smart Home's 60,000 m³/h thermal oxidation facility demonstrates FluxFine's unique mastery over difficult, oil-laden industrial VOC streams that defeat standard thermal equipment.
Whether replacing unworkable legacy scrubbers, executing structural rooftop retrofits with zero downtime to active production, or engineering auto-thermal recovery matrices that eliminate auxiliary fuel consumption, FluxFine provides global HVAC and appliance manufacturers with proven, certified turnkey solutions.
Equipment in This Project
Three-Tower RTO
A premier-grade industrial VOC thermal abatement system that achieves >=99% VOC destruction efficiency and >=95% thermal energy recovery through a classic three-bed alternating heat-exchange and purge process.
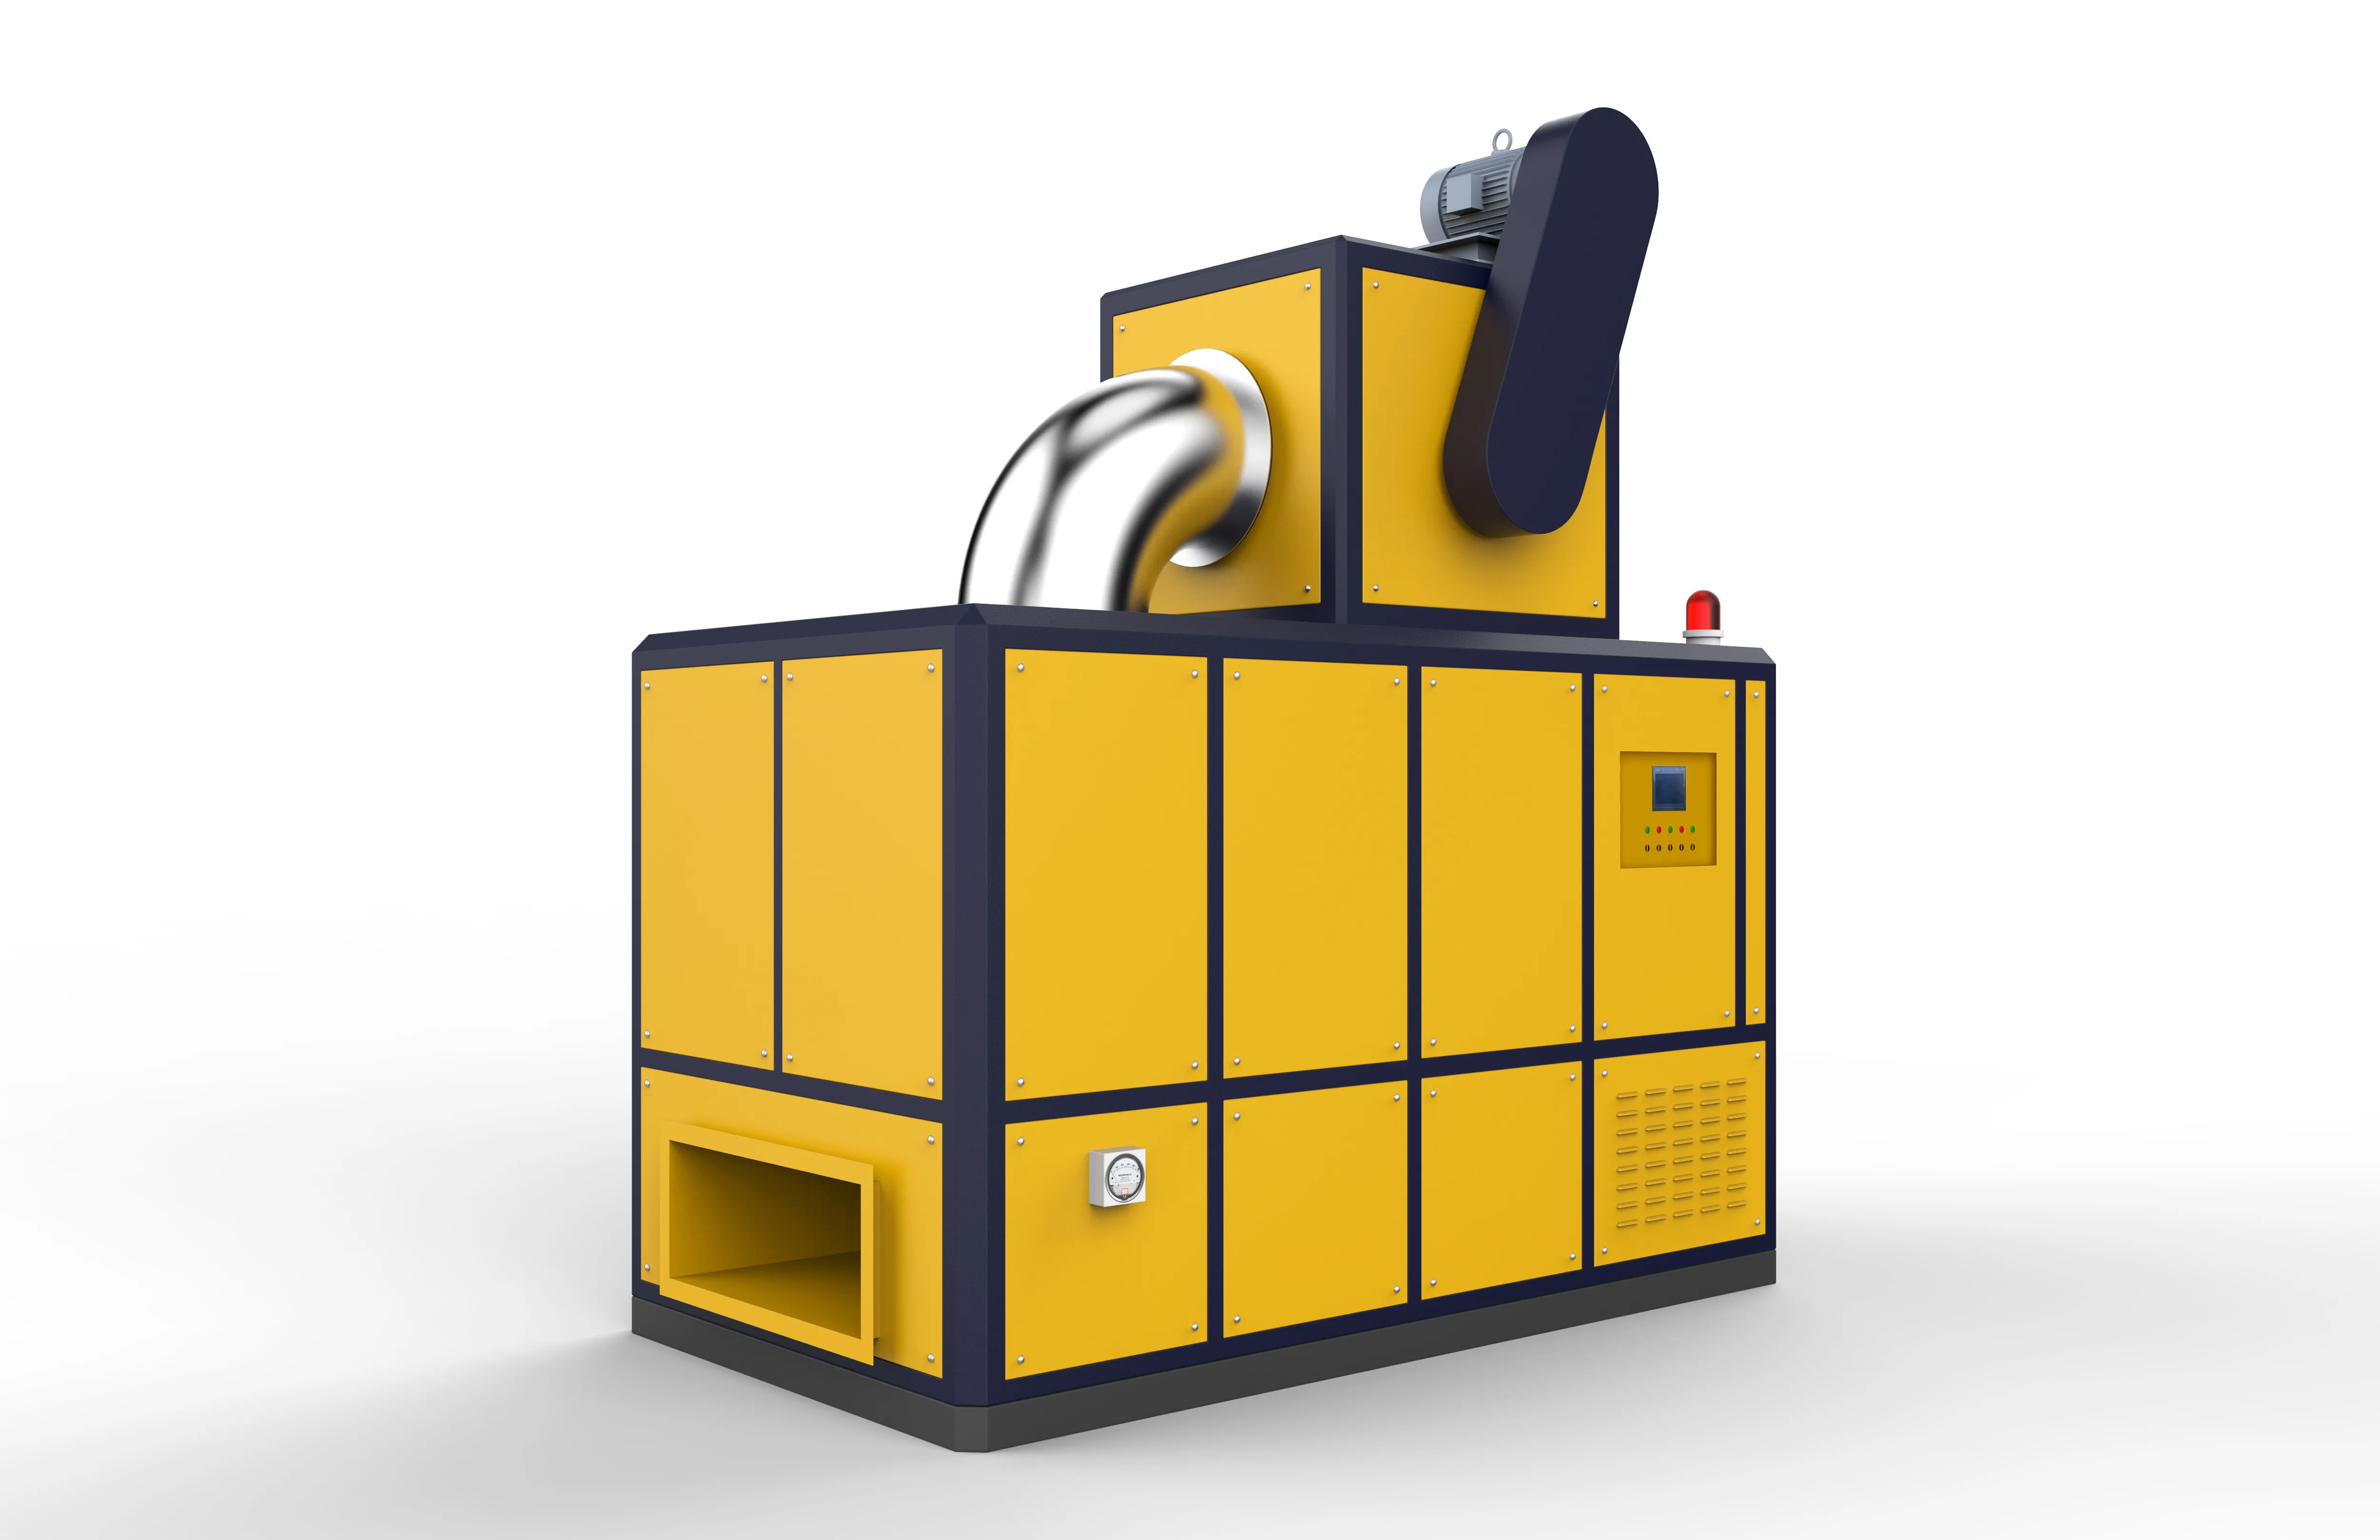
304 Stainless Air Duct
High-quality 304 stainless steel welded air ducts with anti-corrosion coatings, sized 80-2000mm.
Ready to Eliminate Stamping Oil VOCs & Cut Thermal Fuel Costs?
Connect with our senior environmental engineers. We evaluate your furnace exhaust conditions, oil mist loading, and roof structural capacities to deliver guaranteed compliance and minimum OPEX.