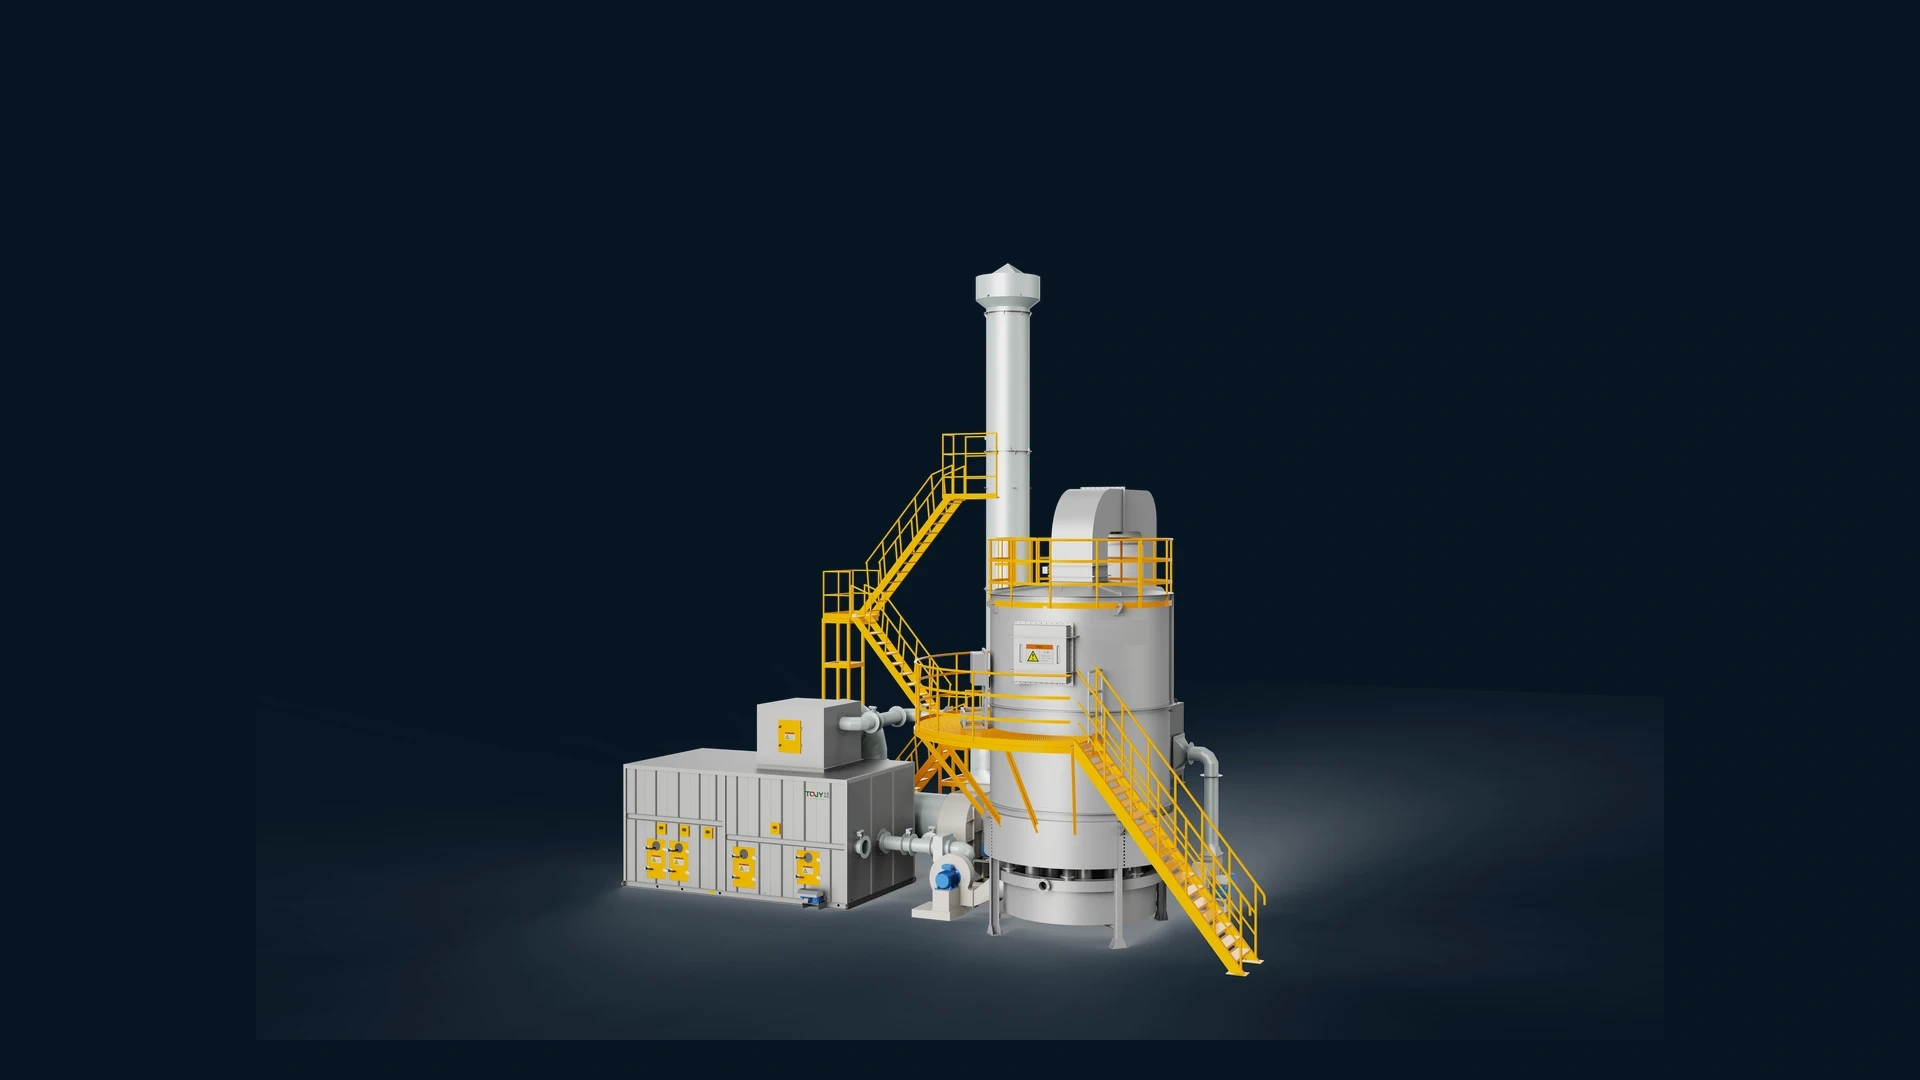
127,000 m³/h Protective Coating & Chemical VOCs Abatement System
Sanhe Industrial Group (HKEX: 3010) | Heavy-Duty Protective Paints, Aerosol Chemicals & Synthetic Resins
Corrosion-Resistant Decoupled Oxidation for Complex Chemical & Coating Exhaust
Sanhe Fine Chemical Group Co., Ltd. (三和精化集团有限公司, HKEX: 3010 / 广东三和) is an internationally recognized publicly listed chemical manufacturer specializing in high-performance automotive aerosols, heavy-duty anti-corrosive coatings, synthetic architectural paints, and industrial adhesives. Manufacturing operations generate dual-stream exhausts totaling 127,000 m³/h (74,700 CFM) from reactor kettles, high-speed dispersion tanks, filling lines, and storage vents.
The production exhaust carried severe technological risks: the presence of dodecylbenzenesulfonic acid, an active surfactant that transforms into corrosive SO₂ and sulfurous acid upon thermal oxidation, threatening premature metal shell perforation and ceramic block degradation; additionally, siloxanes from antifoam agents risk irreversible silica (SiO₂) vitreous fouling on heat-recovery honeycombs.
FluxFine executed a comprehensive turnkey EPC retrofit: deploying an automated counter-flow alkali wet scrubber for sulfur neutralization, a 4-stage modular dry filtration box (G4/F7/F9 plus sacrificial carbon guard), a 100,000 m³/h Zeolite Rotor Concentrator (12.5:1 ratio), and a centralized 35,000 m³/h Three-Bed Regenerative Thermal Oxidizer (3-Bed RTO) treating the merged oven exhausts and desorption stream. The unit delivers guaranteed DRE of ≥98.5% (field operating performance ≥99.2%), completely protects the RTO from acidic corrosion, and achieves stack emissions of NMHC ≤ 30 mg/m³, outperforming national GB 37824-2019 standards.
Four Engineering Dilemmas in Heavy-Duty Paint & Chemical Exhaust
Treating multi-product chemical coating exhaust demands neutralizing acidic corrosion precursors, avoiding silica blinding, and managing large airflow swings.
Sulfuric Acid Corrosion
Formulations include dodecylbenzenesulfonic acid surfactants. Direct oxidation creates SO₂ that forms sulfurous acid condensate, causing rapid metal perforation on RTO chambers.
Silica Fouling Threat
Silicon-based defoaming agents break down into vitreous silica (SiO₂) powder at 800°C+, glassifying ceramic honeycombs. Siloxane streams required strict segregation.
Massive 127,000 m³/h Flow
Ventilation combines 100,000 m³/h of dilute room air (200 mg/m³) with 27,000 m³/h of reactor vents (1,000 mg/m³). Sizing a single direct RTO would be cost-prohibitive.
Surplus Enthalpy Venting
During heavy aerosol canning runs, solvent concentration surges create extreme heat release in the RTO. Automated high-temperature bypass dampers were required for over-temp relief.
Comparative Audit: Scheme 1 (Legacy Patch) vs. Scheme 2 (Unified Turnkey Train)
FluxFine evaluated retaining deteriorated legacy units against engineering a unified 127,000 m³/h concentration and thermal oxidation train.
| Engineering Dimension | Scheme 1: Legacy Retain & Patch | Scheme 2 (Adopted): Unified Turnkey Train | Engineering Rationale |
|---|---|---|---|
| Acid Corrosion Resistance | No alkali tower; severe ongoing sulfur corrosion on RTO shell | Alkali counter-flow spray scrubber neutralizing 100% of acid mist | Zero acid corrosion risk |
| RTO Thermal Core | Aging, corroded legacy unit with dropping thermal efficiency | New 35,000 m³/h Three-Bed RTO with structured cordierite media | ≥95% TER efficiency |
| Pre-filtration Architecture | Simple filter mats prone to particulate bypass | 4-stage dry box (G4+F7+F9+Active Carbon sacrificial guard) | >99% mist & high-boiler capture |
| Destruction Efficiency (DRE) | Unstable 85.0% - 90.0% due to valve seal deterioration | ≥98.5% guaranteed (measured field performance ≥99.2%) | ≥99.2% verified DRE |
| Compliance Assurance | High risk of catastrophic failure during environmental audit | Continuous stack NMHC ≤ 30 mg/m³ (GB 37824-2019 Table 2) | 100% compliance record |
Complete high-temperature thermal destruction across 35,000 m³/h Three-Bed RTO.
Strictly compliant with GB 37824-2019 Table 2 specialized chemical standards (≤ 50 mg/m³).
Alkali counter-flow scrubber prevents sulfurous acid corrosion on RTO ceramic beds.
Compresses 100,000 m³/h dilute room air into 8,000 m³/h concentrated stream for RTO entry.
Subsystem Architecture & Hardware Execution
Explore the four synchronized engineering subsystems delivering acid neutralization, aerosol interception, and high-efficiency regenerative thermal oxidation.
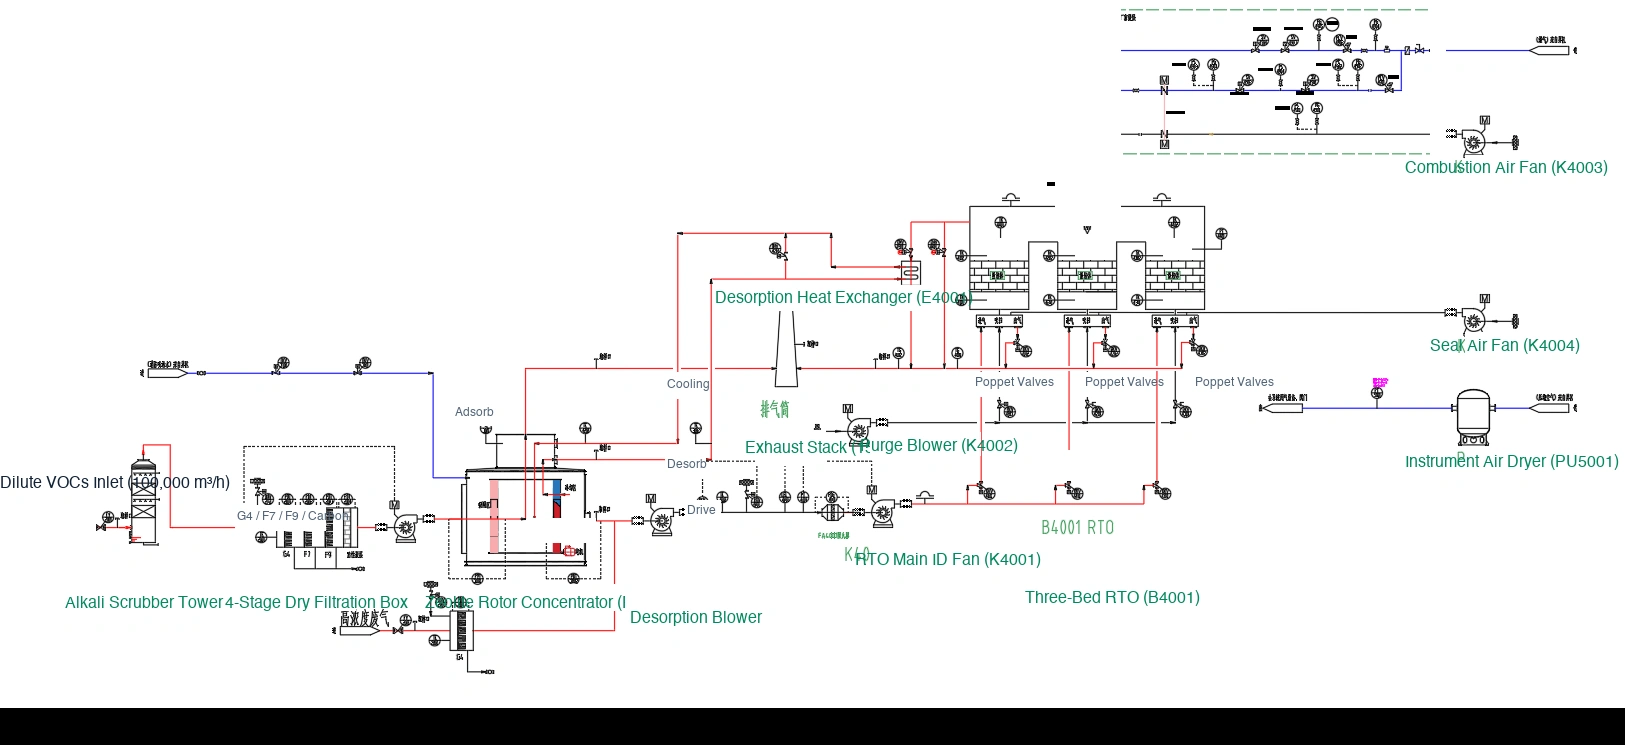
Complete Plant Layout & Unified RTO Architecture
Under the unified Scheme 2 layout, deteriorating legacy units were dismantled and replaced by a consolidated 127,000 m³/h treatment train.
100,000 m³/h of dilute workshop exhaust undergoes alkaline scrubbing and four-stage dry filtration before entering the 100,000 m³/h zeolite rotor. The 8,000 m³/h concentrated desorption stream merges with 27,000 m³/h of reactor kettle exhaust into the 35,000 m³/h Three-Bed RTO.
Parameters: 100,000 m³/h zeolite flow; 27,000 m³/h direct oven flow; 35,000 m³/h RTO capacity; 800°C–850°C combustion setpoint.
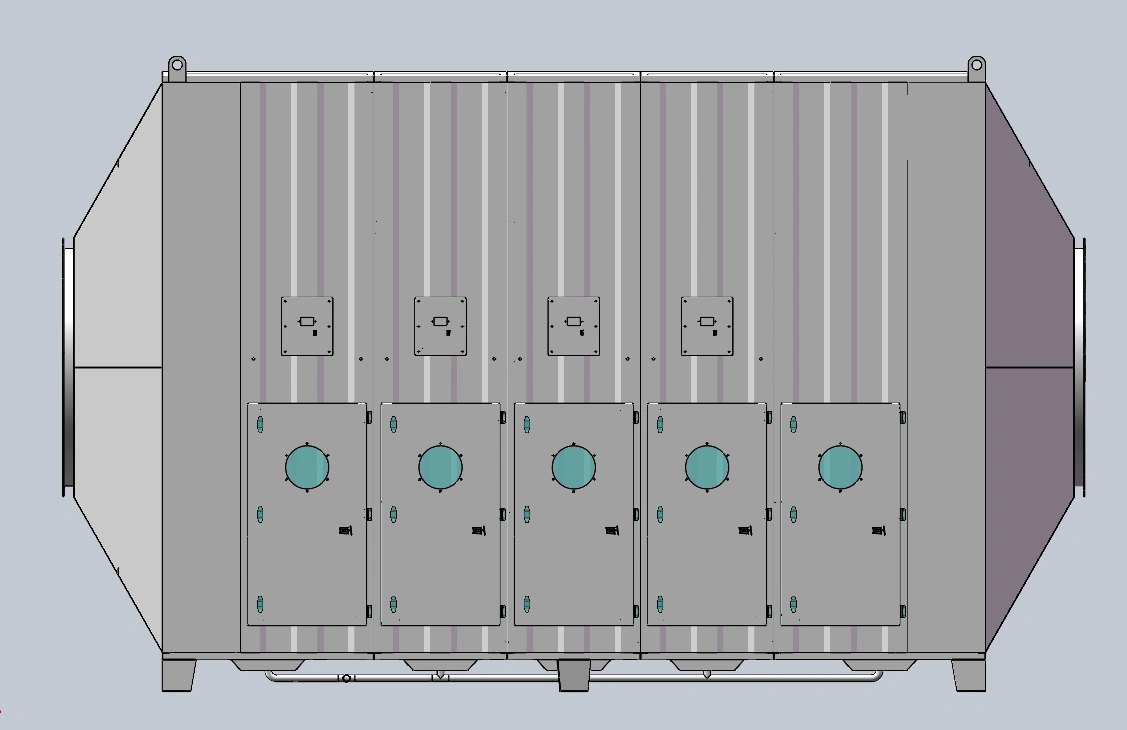
Counter-Flow Alkaline Scrubbing & Modular Pre-Filtration
To neutralize corrosive dodecylbenzenesulfonic acid surfactants before reaching high-temperature combustion, exhaust passes through a heavy-gauge PP counter-flow alkaline scrubber tower.
Circulating NaOH solution (pH 8.5–10.0) atomized through non-clogging spiral nozzles reacts with acid precursors, converting them into soluble neutral salts while knocking down water-soluble aerosols and condensables.
Parameters: Gas velocity 1.8–2.2 m/s; liquid-to-gas ratio 2.5 L/m³; droplet eliminator mist carryover <20 mg/m³; automatic pH dosing system.
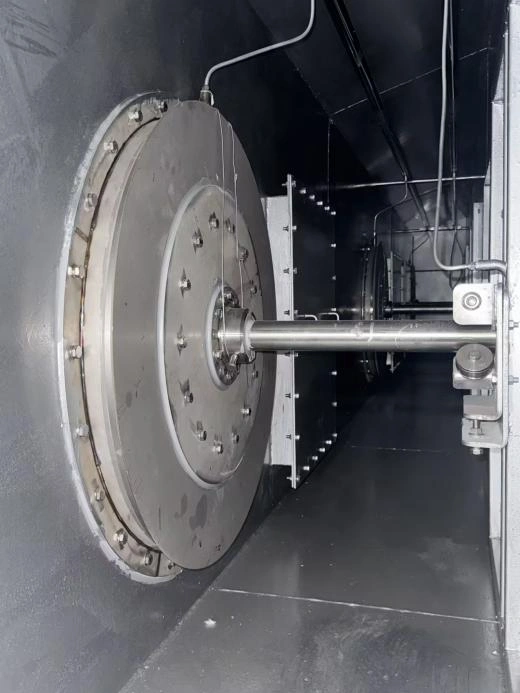
Poppet Valve Actuation & Zero-Slip Purge Cycle
The Three-Bed RTO utilizes high-speed pneumatic poppet switching valves driven by heavy-duty SMC actuators with feedback positioners. The rapid ≤1.0s switching stroke minimizes flow perturbation.
Before switching a regenerative bed from inlet preheating to outlet heat recovery, a dedicated clean air purge sweeps raw solvent vapors back into the combustion chamber, completely eliminating transient switching bypass slips and ensuring ≥98.5% DRE.
Parameters: Valve leakage rate ≤0.05%; 120 N·m actuator torque; ≤1.0s cycle transition time; 1,000,000-cycle industrial endurance rating.
System Operational & Thermodynamic Data Matrix
Verified operational thresholds, airflow capacities, and destruction metrics for the Sanhe Industrial Group facility.
| Subsystem | Design Specification | Operating Metric | Compliance Standard |
|---|---|---|---|
| Three-Bed RTO Thermal Core | 35,000 m³/h three-chamber regenerative thermal oxidizer | 760°C - 850°C oxidation setpoint; ≥1.0s residence | ≥98.5% guaranteed DRE |
| Zeolite Rotor Concentrator | 100,000 m³/h continuous hydrophobic molecular sieve drum | 12.5:1 concentration ratio (100,000 to 8,000 m³/h) | ≥92.0% adsorption efficiency |
| Counter-Flow Alkali Scrubber | PP vertical absorption tower with automated NaOH dosing | 100% sulfur precursor neutralization | Zero acid corrosion on RTO |
| Four-Stage Dry Filtration Unit | G4 panel + F7 pocket + F9 fine + sacrificial active carbon bed | ΔP ≤ 450 Pa clean resistance | High-boiler and aerosol interception |
| Thermal Energy Recovery (TER) | Structured cordierite ceramic honeycomb media | ≥95% thermal recovery efficiency | Auto-thermal at ≥1,800 mg/m³ |
| Stack Emissions (NMHC) | Continuous flame ionization detector (FID) monitored | Measured ≤ 30 mg/m³ | GB 37824-2019 Table 2 (≤ 50 mg/m³) |
Equipment in This Project
Three-Tower RTO
A premier-grade industrial VOC thermal abatement system that achieves >=99% VOC destruction efficiency and >=95% thermal energy recovery through a classic three-bed alternating heat-exchange and purge process.
Zeolite Rotor
A high-efficiency VOC pre-treatment and concentration system utilizing advanced hydrophobic zeolite molecular sieves to continuously adsorb, desorb, and enrich large-airflow, low-concentration organic exhaust gases, reducing downstream thermal destruction energy consumption by 40% to over 50%.
Rotor + 3-Tower RTO
The premier system for large-airflow, low-concentration VOC emissions, combining a hydrophobic zeolite rotor for 10-40x gas enrichment with a mature three-tower RTO for complete destructive oxidation, cutting energy costs by 40%-60%.
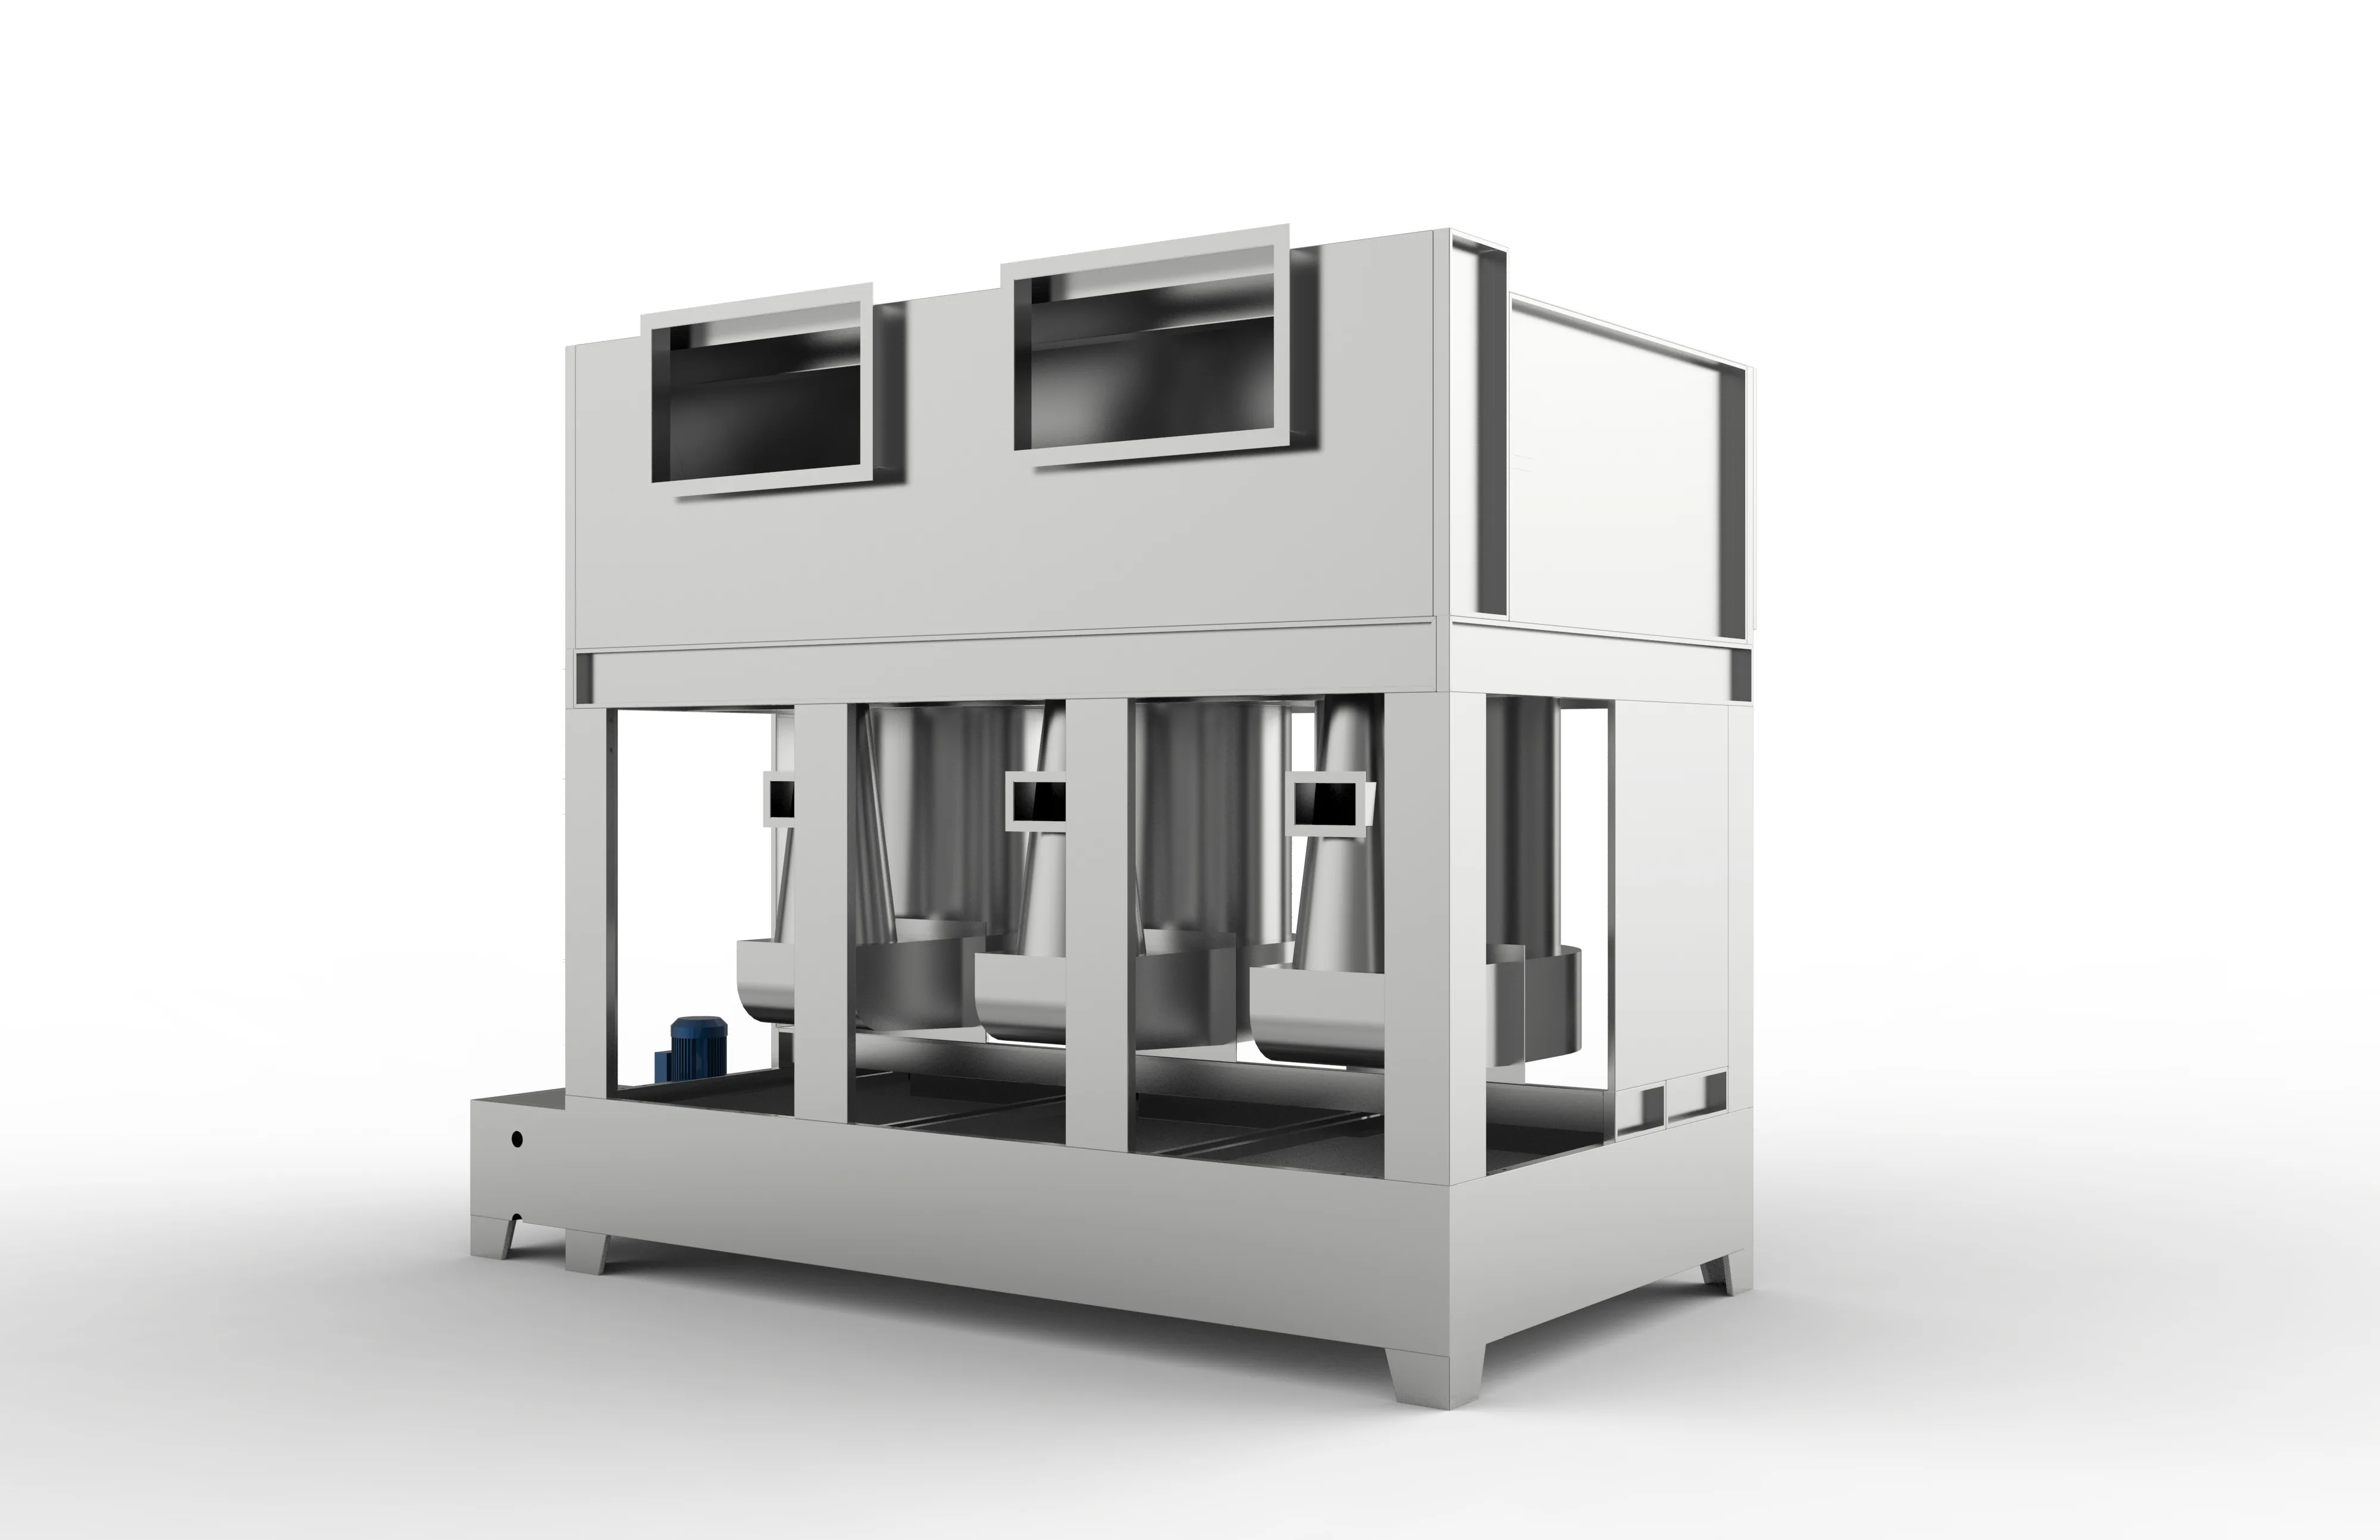
Spray Tower
Custom-built packed spray towers in PP or 304 SS for neutralizing acidic, alkaline, and water-soluble waste gases.
Corrosion-Resistant VOC Abatement for Heavy-Duty Chemical & Paint Plants
FluxFine engineers robust turnkey air pollution control systems incorporating alkaline pre-scrubbing, high-capacity zeolite concentration, and heavy-duty regenerative thermal oxidizers.